254 SMO Instrumentation Valves (UNS S31254 / 6-Moly Super-Austenitic)
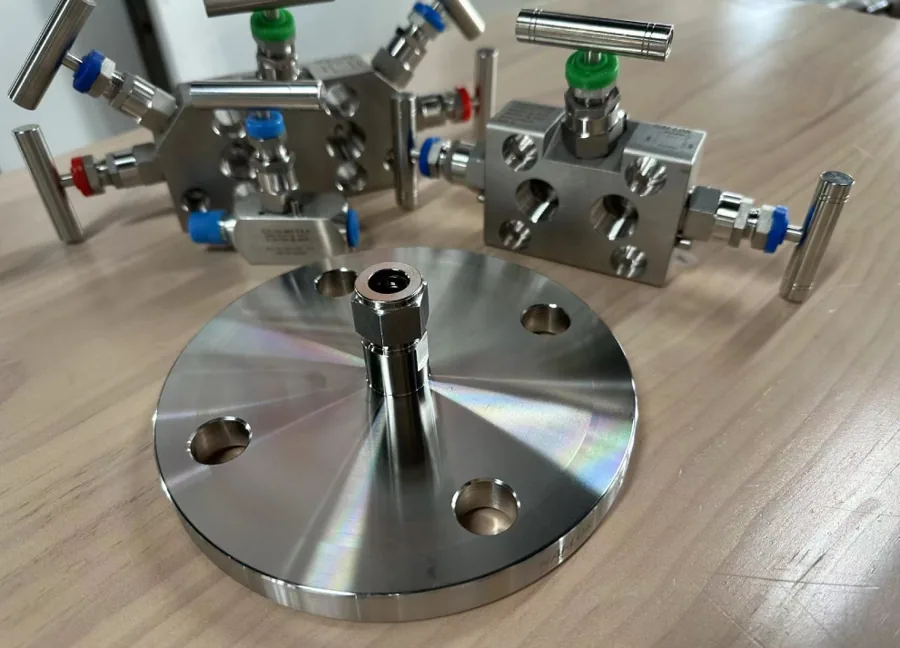
254 SMO instrumentation valves are small-bore isolation, throttling, and block-and-bleed valves machined from UNS S31254, a 6% molybdenum super-austenitic stainless steel (W.Nr. 1.4547, nominally 20Cr-18Ni-6Mo with about 0.2% nitrogen and a small copper addition). Crestflo builds the whole valve family in this grade: needle, ball, check, 2/3/5-valve manifolds, monoflange, double block-and-bleed, and bleed valves, sized 1/16-inch through 1-inch. You reach for a 254 SMO body and trim when the line carries seawater, chloride brine, bleach or chlorine-dioxide liquor, or acidic FGD condensate, the high-chloride duty where 316 pits and cracks and even 904L is running out of margin. With a PREN around 43 the alloy delivers seawater-grade pitting and crevice resistance in a fully austenitic, non-magnetic form. Design follows ASME B16.34, sour-service builds are offered to NACE MR0175 / ISO 15156, and seat and shell leak testing follows the applicable API 598 / BS EN 12266 practice. Standard items ship from stock; specials are built to order, with delivery running 6-8 weeks. Request a quote to price your configuration.
254 SMO® is a registered trademark of Outokumpu OYJ. Swagelok®, Parker®, and Hy-Lok® are trademarks of their respective owners; Crestflo is not affiliated, and interchange is dimensional.
Why Specify a 254 SMO Valve Body and Trim
A valve is a harder corrosion problem than a straight run of tube. The media sits trapped in body cavities, dead legs, and the packing bore. It cycles across the seat. It concentrates in crevices under the stem and in thread roots. That is exactly the geometry where chloride pitting, crevice attack, and chloride stress-corrosion cracking start, so a valve in the wrong alloy fails long before the pipe around it does: on a seawater line, a 316 valve pits out in the stem crevices and seat pocket while the tube still looks fine.
254 SMO is a 6% molybdenum, nitrogen-alloyed super-austenitic stainless, and that chemistry is the whole reason to specify it for a valve in chloride service. The molybdenum and nitrogen together drive pitting and crevice resistance, giving a PREN near 43, roughly double the ~24 of 316L and a clear step above the ~34 of 904L. In practice the valve resists localized chloride attack at temperatures where those lower-moly grades pit in the seat pocket and under the packing. The high nickel and fully austenitic structure resist chloride stress-corrosion cracking, the failure mode that most often retires 304 and 316 stems in warm chloride service, and the copper addition adds useful resistance in reducing acids such as sulfuric. For a valve that sees seawater, chlorinated cooling water, bleach liquor, or FGD scrubber condensate, that is the difference between a valve that keeps sealing and one that seizes.
Be precise about where 254 SMO sits against the neighbors, because it is easy to over- or under-specify a valve body. In chloride pitting resistance 254 SMO is in the same tier as super-duplex 2507 (PREN ~43) and just below AL-6XN (UNS N08367, PREN ~45-47), the other common 6-moly super-austenitic that runs slightly higher molybdenum and nitrogen. The difference against duplex is structural: 254 SMO is fully austenitic, so a 254 SMO valve is non-magnetic in the annealed condition, welds and machines more forgivingly, and keeps its toughness down to cryogenic temperatures with no ductile-to-brittle transition. Super-duplex 2507 carries roughly double the yield strength but is ferromagnetic, so where a thin-wall, high-pressure body needs strength-per-wall, 2507 is the better call, and where magnetic permeability or sub-zero toughness matters, 254 SMO wins. One honest limit: 254 SMO is a corrosion-resistant grade, not a high-temperature strength alloy. Above roughly 750°F (400°C) it risks intermetallic precipitation, so a hot acid or high-temperature line is a signal to step up to a nickel alloy such as Hastelloy C-276 or Inconel 825, not to push 254 SMO past its band. The full metallurgical picture, composition ranges, mechanical and physical properties, PREN, and corrosion-by-media data, lives on the 254 SMO alloy grade page. This page stays on the valve.
Also Specified As: 254 SMO Needle Valve, UNS S31254 Ball Valve, 6Mo Manifold Valve
Buyers and specifiers call these valves several ways, and they all point to the same 6% molybdenum super-austenitic. A requisition might read "254 SMO needle valve," "UNS S31254 ball valve," "6Mo valve," "254 SMO manifold valve," "S31254 instrument valve," or just "6-moly manifold," and each one lands here. 254 SMO® is the Outokumpu trade name (originally Avesta 254 SMO); Alloy 254, SMO 254, 6Mo, and 6-moly stainless are the generic forms. The material is registered as UNS S31254 and EN / Werkstoff 1.4547, with ASTM forging/flange grade F44 (A182 F44). One caution worth keeping on the PO: 254 SMO is not 253 MA, which is a heat-resistant austenitic grade for high-temperature service, a different alloy for a different job.
Scope: these are instrumentation valves, the small-bore kind that isolate and throttle gauge, transmitter, analyzer, impulse, and sample lines. A ball valve here means an instrument ball valve, not a plumbing valve; a needle valve means a flow-metering instrument valve, not a carburetor part; a manifold means a valve manifold, not an exhaust or PEX manifold. "6-moly" refers to the molybdenum content of the alloy, not a plumbing part.
254 SMO Valve Types: Needle, Ball, Check, Manifold, Monoflange & DBB
Crestflo machines the full instrumentation valve family in 254 SMO, so you can standardise an entire hookup, primary isolation through bleed, on a single seawater-grade alloy. Each type links to its own detail page for dimensions and ordering.
| Valve type | Function in a 254 SMO hookup | Typical service | Detail page |
|---|---|---|---|
| Needle valve | Fine throttling and primary isolation, multi-turn non-rotating tip | Gauge and DP-transmitter roots, calibration, sampling | Needle valve |
| Ball valve (2-way, 3-way, L-/T-port) | Quarter-turn on/off isolation and diverting | Sample shut-off, gauge selection, switching | Ball valve |
| Check valve / NRV | Spring-loaded one-way, non-return flow | Back-flow protection on analyzers and pumps | Check valve |
| 2/3/5-valve manifold | Combined block, bleed, and equalise in one body | DP-transmitter and gauge isolation | 3-valve · 5-valve |
| Monoflange valve | Integral block-and-bleed on a flanged connection | Compact direct-mount gauge/transmitter isolation | Monoflange |
| Double block-and-bleed (DBB) | Two blocks plus a bleed in one body, per ASME B16.34 | Positive double isolation, custody and hazardous lines | DBB valve |
| Bleed / vent valve | Small stem bleed to vent, drain, or depressurise | Manifold bleed ports, gauge venting | Bleed valve |
Beyond these, 254 SMO is available in gauge/root, metering, toggle, plug, relief, and packless (bellows and diaphragm) patterns, and the grade also covers regulator bodies for chloride service. Spell out the function on the RFQ and the engineering team confirms the build. For the complete family and the specialty patterns, start at the instrumentation valves pillar.
254 SMO Manifold Valves: 2-, 3- & 5-Valve for DP Transmitters
The manifold is where 254 SMO earns its keep on a seawater, brine, or FGD DP measurement. A 3-valve manifold gives you two block valves plus an equalise valve to protect the transmitter cell during zeroing; a 5-valve adds two bleed/vent valves for calibration and purging. Crestflo builds these in 254 SMO with non-rotating stem tips to protect the seat, and every manifold gets 100% seat and shell leak testing before it ships. Direct-mount and remote-mount patterns both carry over to the alloy. On a chloride-laden DP tap, the trapped media sitting in the block cavities is exactly what pits a 316 manifold out from the inside; the 254 SMO body keeps that from becoming the failure point.
Actuation: Manual and Pneumatic 254 SMO Valves
Most instrumentation 254 SMO valves are hand-operated, bar-stock or forged-body construction, with the handle chosen for the duty: lever and phenolic or metal T-bar handles on ball valves, vernier and locking/lockout handles where throttling repeatability or line-identification matters, and color-coded handles for service marking. Because 254 SMO is non-magnetic, it is a natural fit where stray magnetic fields or permeability are a concern on the instrument rack. Where a line needs remote or automated operation, ball and needle patterns are available with pneumatic actuation. Panel-mount and low-profile builds support instrument-rack and enclosure installations.
Seat & Packing Materials for Seawater, Chloride & FGD Service
The 254 SMO body and trim handle the corrosion; the soft-goods set the temperature ceiling and the seat-leakage class. This is the choice that most often gets a 254 SMO valve wrong, picking a packing that can take the chemistry but not the heat, or the reverse. The seat and stem-seal options below pair with a 254 SMO body, and the temperature limits are the standard published limits for each material. Confirm the certified rating for your build on the RFQ.
| Seat / packing material | Typical temperature limit | Why choose it |
|---|---|---|
| PTFE (virgin) | up to ~450°F (232°C) | Default soft seat, excellent chemical resistance, tight bubble-tight shut-off |
| Reinforced / glass-filled PTFE (RTFE) | up to ~450°F (232°C) | Higher load capacity and cold-flow resistance than virgin PTFE |
| PCTFE | cryogenic to ~250°F (121°C) | Low-temperature and gas service where PTFE creep is a concern |
| PEEK | up to ~600°F (315°C) | High-pressure, higher-temperature throttling with good chemical resistance |
| Graphite (flexible, Grafoil-type) | material limit ~850°F (454°C); capped by the 254 SMO body at ~750°F (400°C) | High-temperature stem packing, up to the alloy's own ceiling |
| Metal-to-metal seat | limited by the 254 SMO body (to ~750°F / 400°C) | Severe-cycling throttling near the alloy's upper band, where soft seats cannot survive |
For seawater and chloride duty the usual pairing is a 254 SMO body and trim with reinforced PTFE, where a bubble-tight soft seat matters and the temperature sits in the moderate band most chloride service lives in. The point of 254 SMO is that the metal in contact with the media does not become the weak link; the soft-good choice then tunes the valve to the temperature and the leak class. Note the body ceiling here: unlike the nickel alloys, 254 SMO is a corrosion grade, not a high-temperature strength alloy, so its roughly 750°F (400°C) limit caps the hottest builds and even the graphite packing cannot be run past it. A line hotter than that is a signal to look at a nickel-alloy valve instead. Seat and packing figures follow the applicable standard and are customisable to requirement.
254 SMO Valve Sizes (1/16″–1″) & End Connections: NPT, BSPP, Tube & Weld
254 SMO instrumentation valves ship in imperial fractional sizes from 1/16-inch to 1-inch and in a matching metric menu, with the port and end connection configured to the hookup. Tube-fitting (compression) ends land as single or double ferrule and interchange dimensionally with the major brands; threaded ends follow published thread dimensions and can be tailored. Because 254 SMO is a tough, work-hardening super-austenitic that can gall on threaded and stem surfaces, Crestflo applies anti-galling measures such as silver plating on request where repeated make-up or high torque is expected.
| Attribute | Options | Standard |
|---|---|---|
| Size range | 1/16″, 1/8″, 1/4″, 3/8″, 1/2″, 3/4″, 1″ (imperial); metric menu | Imperial and metric |
| Tube-fitting ends | Compression, single or double ferrule | Dimensional interchange with major brands |
| Tapered pipe threads | NPT (male/female), NPTF, BSPT | ASME B1.20.1 (NPT); BSP |
| Parallel pipe threads | BSPP / ISO parallel | ISO parallel |
| Flare / port | SAE / JIC 37°, SAE ORB | Per applicable standard |
| Welded ends | Socket-weld, butt-weld | Per applicable standard |
| Flanged ends | On DBB and monoflange builds | ASME flange standards |
Port configuration, bore, and Cv depend on the valve type and size; the engineering team confirms the orifice and flow coefficient for your pattern at quotation. Values per applicable standard; customisable to requirement.
Pressure & Temperature Ratings for 254 SMO Instrumentation Valves
Pressure rating is set by the valve design and its governing standard, not by the alloy. Manifolds are rated up to 10,000 psi and double block-and-bleed valves to 3,000 psi under ASME B16.34; other types carry their own ratings on their detail pages, and higher-pressure requirements are handled on the high-pressure line. The temperature ceiling is the lower of two limits: what the 254 SMO body can take and what the seat and packing material allows. 254 SMO holds strength and toughness from cryogenic temperatures up to roughly 750°F (400°C) for continuous service, a lower ceiling than the nickel alloys because 254 SMO is a corrosion-resistant grade rather than a high-temperature strength alloy; above that band it risks intermetallic precipitation. In most seawater and chloride service the real line temperature sits well under that figure and the soft-good packing sets the practical limit, with the body ceiling only governing on a metal-seated valve near the top of the band. Confirm the exact certified rating for your build on the RFQ.
| Valve type | Max pressure | Rating basis |
|---|---|---|
| 2/3/5-valve manifold | up to 10,000 psi | ASME B16.34 |
| Double block-and-bleed | up to 3,000 psi | ASME B16.34 |
| Needle, ball, check & other patterns | Type- and design-specific; confirmed per configuration | ASME B16.34 / applicable API standard |
| Higher-pressure builds | See the high-pressure line | Per applicable standard |
Standards, Testing & NACE MR0175 Sour-Service Compliance
A valve's pressure boundary and its seat are qualified against different standards than a fitting is, and 254 SMO valves follow the valve standards, not the compression-fitting standard. Pressure-boundary design follows ASME B16.34. Seat-leakage and pressure testing follow the applicable API 598 / BS EN 12266 regime for the valve type. For sour service, 254 SMO valve material is offered to NACE MR0175 / ISO 15156: in the solution-annealed condition, UNS S31254 is used in sour (H₂S-containing) service within the limits of NACE MR0175 / ISO 15156; confirm the hardness, H₂S partial pressure, chloride, and temperature limits in the standard against your application before committing. Crestflo holds the standard approvals that apply to instrumentation valves.
| Standard | Scope | Applies here |
|---|---|---|
| ASME B16.34 | Valve pressure-boundary design and pressure-temperature rating | Yes |
| API 598 / BS EN 12266 | Valve inspection and seat/shell leak testing | As applicable to type |
| NACE MR0175 / ISO 15156 | Sour-service material requirements | Sour-service builds |
| ASME B1.20.1 | NPT thread dimensions | Threaded ends |
| EN 10204 MTC 3.1 / 3.2 | Material test certification | Yes |
| ISO 9001 / 14001 / 45001 & PED | Quality, environmental, safety, pressure | Certified |
Every valve runs through a deep test battery: hydraulic proof, burst, and impulse; pneumatic; flexure-fatigue, rotary-flex, vibration, and thermal-cycling work; plus pull-out and vacuum checks. Hydrostatic shell and seat-leak testing verify the pressure boundary and the shut-off, and helium leak testing is available where a gas-tight, low-fugitive seal must be proven. Positive material identification (PMI) confirms the alloy on every part, which matters on a 6-moly super-austenitic, where the molybdenum, nitrogen, and nickel content is exactly what buys the chloride performance and an under-alloyed substitute looks identical but pits in service. Non-destructive testing is done in-house. Manifolds all get 100% seat and shell leak testing. Destructive testing goes out to ISO/IEC 17025-accredited labs, and third-party inspection is available on request.
Material Traceability & Certification
Every 254 SMO valve carries its own heat/lot number, and each order ships with an EN 10204 MTC 3.1 certificate as standard, with 3.2 available on request. PMI confirms the grade at the part level, every time. That documentation backs the audit trails that offshore, desalination, and chemical-plant jobs demand. On a 6-moly, under-alloying is the specific risk: a valve quietly supplied as 316 or a leaner grade looks identical but pits in chloride service. Because 254 SMO work-hardens and machines tougher than standard stainless, Crestflo keeps the work in-house on CNC, VMC, and EDM equipment to hold the tolerances a leak-tight instrumentation valve needs.
Applications for 254 SMO Instrumentation Valves
254 SMO valves earn their place wherever chlorides outrun what 316 or even 904L can handle, the seawater-grade duty where pitting, crevice attack, and chloride stress-corrosion cracking are the governing failure modes, and the temperature stays below the alloy's band:
- Offshore oil & gas and marine instrumentation, platform instrument hook-ups, hydraulic control lines, and chemical-injection systems exposed to seawater, sea spray, and chloride-bearing produced fluids. See the offshore and seawater industry page.
- Desalination and seawater cooling, SWRO, MSF, and MED plants and seawater cooling-water instrumentation, where raw chloride service defeats standard stainless.
- Pulp & paper bleaching, chlorine-dioxide and bleach-plant lines, among the most aggressive chloride environments in process industry.
- FGD and pollution control, flue-gas desulfurization absorbers and scrubber-condensate instrumentation, where chloride-bearing acidic condensate attacks lower alloys.
- Chemical and coastal processing, mixed chloride and reducing-acid streams, and coastal plant instrumentation where the ambient environment alone is corrosive. See the petrochemical and chemical industry page.
Pairing 254 SMO Valves With 254 SMO Fittings and Tubing
A valve is one part of the hookup. For a corrosion-matched instrument run, pair these valves with 254 SMO tube fittings and 254 SMO tubing so the whole assembly, body, ferrules, and tube, carries the same chloride resistance and the same traceability. Mixing a 254 SMO valve onto 316 tube and fittings just moves the failure point downstream, to the first crevice the seawater finds.
Drop-In Interchange With Swagelok, Parker & Hy-Lok
Crestflo 254 SMO instrumentation valves are built as dimensional interchange / equivalent valves for the major brands, with performance qualified against ASME B16.34 and the applicable API valve standards, not against marketing language. These are not "compatible" or "intermix" parts. Swagelok®, Parker®, and Hy-Lok® remain trademarks of their respective owners, and Crestflo is not affiliated; the interchange is strictly dimensional. We don't publish a part-number table. Instead, our engineering team prepares an interchange reference per project: request your cross-reference and we'll map your existing valve part numbers to Crestflo 254 SMO equivalents.
Origin & US-Serving Positioning
Crestflo manufactures for the US market. Standard product comes from India; US or European melt is available on request, with full material traceability. Valves are engineered as US drop-in replacements and ship in 6-8 weeks, well under the 20+ weeks typical of the majors. If a project calls for a specific melt origin or TAA/DFARS handling, specify it on the RFQ, and we'll address it straight. We never claim "made in USA."
Why Crestflo for 254 SMO Valves
Crestflo operates as the instrumentation division of an export house with four decades behind it and formal recognition from the Government of India, with a proven Middle-East delivery record. That backing grounds a focused instrumentation brand built on a handful of clear advantages:
- Lead time of 6-8 weeks versus 20+ weeks typical of the majors.
- The full valve family in one alloy, needle, ball, check, manifold, monoflange, and DBB, all in 254 SMO.
- Small MOQ and private label for distributors and OEMs.
- Both imperial and metric sizing, with the seat and packing tuned to your temperature and leak class.
- Heat-number marking plus MTC 3.1/3.2 on every order, PMI-confirmed against under-alloying, with 100% seat and shell leak testing on manifolds.
- ISO 9001 / 14001 / 45001 & PED certified, cost-competitive after US duties and tariffs.
We Engineer Confidence.
Request a Quote for 254 SMO Valves
Give us the details: valve type, size, port and end connections, seat and packing, and the line conditions (media, pressure, temperature, sour-service requirement). We'll confirm the rating, build it to order, and schedule it.
- Request a quote, the fastest path to pricing and lead time.
- Request your Swagelok®/Parker® valve cross-reference and we'll map your part numbers.
Datasheets and CAD models are available to customers on request. Reach Crestflo's US sales desk at sales@crestflousa.com or +1 346 594 9005 (Houston, TX). Round out the system with 254 SMO tube fittings and 254 SMO tubing, and see where these valves serve in offshore and seawater and chemical processing.
Frequently Asked Questions
What is a 254 SMO instrumentation valve?
It's a small-bore isolation, throttling, or block-and-bleed valve, needle, ball, check, manifold, monoflange, or DBB, with the body and trim machined from UNS S31254, a 6% molybdenum super-austenitic stainless steel (254 SMO / EN 1.4547). The 6% molybdenum and nitrogen give it seawater-grade pitting and crevice resistance (PREN ~43), and its high nickel and austenitic structure resist chloride stress-corrosion cracking, which is why it's specified for seawater, chloride brine, bleaching, and FGD service where 316 and even 904L trim pit, crack, or seize. It is fully austenitic and so non-magnetic in the annealed condition.
Why use 254 SMO instead of 316 or 904L for valve trim?
Because a valve concentrates corrosion where stainless is weakest: trapped media in body cavities, cyclic seat contact, and crevices at the stem and threads. In seawater, chlorinated cooling water, brine, bleach liquor, and FGD condensate, 316 and even 904L trim can pit, crack, or seize. 254 SMO's 6% molybdenum plus nitrogen pushes PREN to about 43, well above 316L's ~24 and a clear step over 904L's ~34, and its high nickel resists chloride stress-corrosion cracking, so the metal in contact with the media stays the reliable part of the valve.
When should I choose 254 SMO over super-duplex 2507 or AL-6XN for a valve?
All three handle seawater-grade chloride service. 254 SMO and super-duplex 2507 sit at about the same PREN (~43), so chloride pitting resistance is comparable, but 2507 is a ferromagnetic duplex with roughly double the yield strength while 254 SMO is a non-magnetic austenitic that welds more forgivingly and stays tough at cryogenic temperatures. Pick 2507 when you need strength-per-wall in a thin, high-pressure body, and 254 SMO when austenitic behavior, non-magnetic character, or sub-zero toughness matters. AL-6XN (UNS N08367) is the near-twin 6-moly super-austenitic, running slightly higher molybdenum and nitrogen (PREN ~45-47), and is the close alternative for the harshest chloride loads. Note the media, temperature, and pressure on the RFQ and we'll confirm the right grade.
Are Crestflo 254 SMO valves NACE MR0175 compliant for sour service?
Yes, within limits. In the solution-annealed condition, UNS S31254 is used in sour (H₂S-containing) service within the limits of NACE MR0175 / ISO 15156. Crestflo offers 254 SMO valve material to that standard with full traceability; confirm the hardness, H₂S partial pressure, chloride level, and temperature limits in the standard against your application, and note the sour-service requirement on the RFQ.
What valve types does Crestflo offer in 254 SMO?
Needle, ball (2-way, 3-way, L-port, T-port), check/NRV, 2/3/5-valve manifolds, monoflange, double block-and-bleed, and bleed valves, plus gauge/root, metering, toggle, plug, relief, and packless bellows/diaphragm patterns, and regulator bodies, on request. Sizes run 1/16-inch to 1-inch in imperial and metric.
What are the pressure and temperature ratings of 254 SMO instrumentation valves?
Pressure is design- and type-specific: manifolds are rated up to 10,000 psi and double block-and-bleed valves to 3,000 psi under ASME B16.34, with other patterns confirmed per configuration. Temperature is the lower of the body limit and the seat/packing limit: virgin and reinforced PTFE to about 450°F (232°C), PEEK to about 600°F (315°C), and the 254 SMO body itself to roughly 750°F (400°C), above which the alloy risks intermetallic precipitation. Because 254 SMO is a corrosion grade rather than a high-temperature strength alloy, that body ceiling caps the hottest builds. Confirm the certified rating on the RFQ.
Which seat and packing materials should I choose for seawater and chloride service?
For seawater and chloride duty, a 254 SMO body and trim with reinforced PTFE suits most lines, where a bubble-tight soft seat matters and the temperature sits in the moderate band chloride service usually lives in. PCTFE suits cold and gas service; graphite packing and metal-to-metal seats handle the hotter, higher-cycle end up to the alloy's own ceiling of about 750°F (400°C). The 254 SMO handles the chemistry; the soft-good is tuned to the temperature and the required seat-leakage class.
Is a 254 SMO valve magnetic?
No. 254 SMO is a fully austenitic stainless steel and is essentially non-magnetic in the annealed condition, unlike super-duplex 2507, which is ferromagnetic. That non-magnetic character, alongside its chloride resistance, is a reason to specify it over a duplex where magnetic permeability matters. Heavy cold work can induce a trace of magnetism, as with any austenitic stainless, but a 254 SMO valve as supplied is non-magnetic.
What standards do 254 SMO valves meet?
Pressure-boundary design follows ASME B16.34, seat and shell leak testing follows the applicable API 598 / BS EN 12266 regime, sour-service material follows NACE MR0175 / ISO 15156, NPT threads follow ASME B1.20.1, and material certification follows EN 10204 (3.1 standard, 3.2 on request). Crestflo manufactures under an ISO 9001 / 14001 / 45001 and PED certified system.
What end connections are available?
Tube-fitting (compression) ends in single or double ferrule, NPT, NPTF, BSPT, BSPP / ISO parallel, SAE / JIC 37° and SAE ORB, socket-weld and butt-weld ends, and flanged ends on DBB and monoflange builds. National, international, and custom threads are supported.
What testing and certification come with the valves?
Each valve carries a heat/lot number and ships with an EN 10204 MTC 3.1 certificate (3.2 on request). PMI confirms the alloy on every part, which matters on a 6-moly where an under-alloyed substitute looks identical but pits. Testing covers hydrostatic shell and seat-leak, hydraulic proof/burst/impulse, pneumatic, fatigue, vibration, thermal cycling, and vacuum, with helium leak testing available; manifolds get 100% seat and shell leak testing. NDT is in-house; destructive testing goes to ISO/IEC 17025-accredited labs, and third-party inspection is available on request.
Do 254 SMO valves interchange with Swagelok, Parker, or Hy-Lok?
They're built as dimensional interchange / equivalent valves, with performance qualified to ASME B16.34 and the applicable API valve standards. They are not "compatible" or "intermix" parts, and every brand name belongs to its respective owner; Crestflo is not affiliated. Send us your valve cross-reference request and we'll map your part numbers.
Are these valves made in the USA?
Crestflo manufactures for the US market. Standard product is of Indian origin, with US or European melt available on request and full material traceability. Valves are engineered for a US drop-in fit and ship in 6-8 weeks. Specify any TAA/DFARS or melt-origin requirement on the RFQ.
What is the lead time and minimum order?
Standard items ship from ready stock; specials are made to order, with a 6-8 week US-serving delivery. Small minimum order quantities apply, and private-label and made-to-print builds are available.
Related Pages
- 254 SMO alloy grade & corrosion data
- 254 SMO tube fittings · 254 SMO tubing
- Instrumentation valves pillar · Needle valve · Ball valve · 3-valve manifold
- Super Duplex 2507 valves · AL-6XN · 254 SMO vs Super Duplex vs AL-6XN
- ASME B16.34 · NACE MR0175 · Offshore & seawater industry · Petrochemical & chemical industry